See us at E-Waste World Expo 2026 ( Booth D136 ) June 17-18th , Messe Frankfurt, Germany
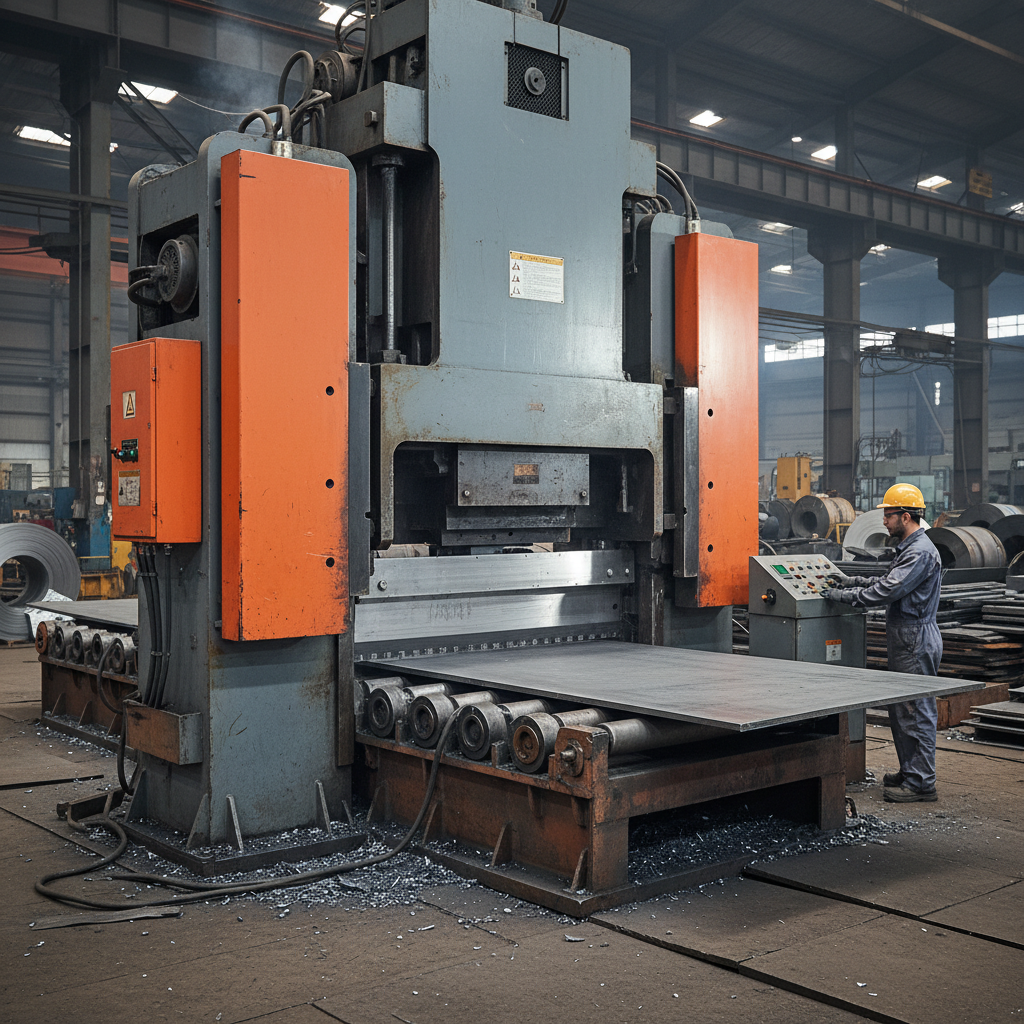
Procuring industrial cutting tools often leads to a common friction point: the disparity between initial purchase cost and long-term operational value. When analyzing shearing machine blade price, many procurement managers focus on the unit cost per piece, overlooking the "hidden" costs of downtime, frequent replacements, and material waste caused by premature blade wear.
The volatility in raw material markets—specifically alloy tool steel and tungsten carbide—coupled with varying precision grinding requirements, means that prices are rarely uniform across the industry. The actual cost of ownership is determined not by the invoice price, but by the blade's performance stability in high-speed production environments, where a 0.1mm deviation can result in thousands of defective parts.
To optimize expenditure, it is essential to move beyond simple price comparisons and instead evaluate blades through the lens of material compatibility, hardness indices, and maintenance cycles. This guide examines the technical drivers of pricing and provides a framework for selecting blades that balance budget constraints with industrial efficiency.


The primary driver of any shearing machine blade price is the metallurgical composition. Standard Alloy Tool Steels, such as 9CrSi, offer a balanced cost-to-performance ratio with a hardness of HRC58-60, making them suitable for low-speed operations and office-grade cardboard. However, for industrial-scale throughput, the shift to Cold Work Die Steels (like SKD-11 or Cr12MoV) increases the price due to higher chromium and molybdenum content, which elevates hardness to HRC61-63 and significantly extends service life.
At the top of the pricing spectrum are Hard Alloys (Tungsten Carbide). With a hardness range of HRA89-93, these materials are designed for extreme wear resistance and high-speed die-cutting (exceeding 100 meters/minute). While the initial cost is substantially higher, the reduction in downtime for sharpening and replacement often justifies the investment in high-volume electronics or energy-sector processing.
Pricing is not solely about raw materials; the manufacturing process—specifically the grinding and finishing stages—adds significant value. High-precision grinding of the blade edge is required to reduce burrs in film-coated cardboard or anti-counterfeiting labels. For instance, achieving a cutting accuracy of ±0.05mm for special-shaped labels requires advanced CNC machining and rigorous quality control, which is reflected in the final cost.
Furthermore, specialized surface treatments influence the price. Titanium plating is often applied to reduce paper debris residue and prevent sticking in adhesive products. Such coatings are critical for maintaining high purity (≥95%) when separating composite films (paper-plastic) and ensuring that the blade does not adhere to the material during high-speed cycles.
The complexity of the blade geometry also plays a role. A simple straight-line knife is more cost-effective than a circular slitting knife (diameters from 100-600mm), which requires precise concentricity and integration with high-performance bearings to function at high speeds without vibration.
One of the most common errors in blade procurement is the pursuit of maximum hardness without considering impact resistance. While tungsten carbide is exceptionally hard, it can be brittle under the high-impact forces associated with cutting heavy corrugated paper or multi-layer cardboard. This is where Cold Work Die Steel (Cr12MoV) becomes the strategic choice.
The optimal selection logic is not based on the highest hardness, but on the matching of material toughness to the specific cutting force; for example, serrated blades with a cutting force ≥500N are essential for heavy cardboard to keep the burr rate below 0.3%.
For manufacturers, this means that a slightly more "affordable" blade made of lower-grade alloy steel may lead to catastrophic failure (chipping) if used in high-impact scenarios, resulting in costs far exceeding the initial savings. Understanding the relationship between the blade angle (typically 15-23°) and the material density is key to maximizing tool life.
To evaluate the true value of a tool, companies should use a relative performance index. A low-cost blade may require sharpening every 8 hours, whereas a high-performance alloy blade might only need inspection every 30 days. When factoring in the cost of labor and the loss of production capacity during tool changes, the "expensive" blade often yields a lower cost-per-cut.
The following index illustrates the relative balance between initial acquisition cost and the resulting operational efficiency (maintenance reduction) across different material grades.
In a typical industrial setting, such as the production of mobile phone protective films or ultra-thin electronic components, the requirement is for a non-contact or laser die-cutting approach to achieve 0.1mm thickness without edge burrs. In these scenarios, the focus shifts from bulk shearing to extreme precision, where the tool's ability to maintain a sharp edge without microscopic chipping is the primary value driver.
Conversely, for high-speed production lines producing over 50,000 pieces of packaging daily, the priority is the reduction of maintenance downtime. In these environments, hard alloy round blades or coated blades are preferred, as they can withstand continuous operation and reduce the frequency of gap adjustments (which must be tightly controlled between 0.03mm and 0.3mm depending on paper thickness).
The industry is moving toward "intelligent" tooling, where the focus is on the synergy between the blade material and the substrate. The rise of new energy battery separators and high-precision electronic packaging has forced a shift toward hard alloy straight-line knives that eliminate delamination.
Changzhou Binsheng Metallurgical Machinery Co., Ltd. exemplifies this transition by integrating ISO 9001 standards with two decades of expertise in metallurgy. By focusing on the Yangtze River Delta's manufacturing cluster, they have refined the use of SKD-11 and Cr12MoV to create tools that last 3-5 times longer than ordinary alloy steel.
Future trends suggest an increase in the use of nano-coatings and hybrid material structures to further bridge the gap between the impact resistance of steel and the wear resistance of carbides, allowing for even higher throughput in recycling and steel mill processing.
When comparing quotes for shearing machine blades, procurement teams should utilize a multi-dimensional matrix. Comparing prices alone is misleading; instead, one must evaluate the material grade, the precision of the edge grinding, and the recommended maintenance interval.
A common trade-off occurs between the initial cost of 9CrSi (high cost-effectiveness for small production) and the long-term value of Tungsten Carbide (essential for high-speed lines). The decision should be driven by the projected total volume of material to be cut over the blade's lifecycle.
The following table provides a technical comparison to assist in selecting the correct tool based on typical industrial requirements.
| Material Type | Hardness Index | Primary Application | Relative Suitability |
|---|---|---|---|
| Alloy Tool Steel (9CrSi) | HRC 58-60 | Office Documents / Low-weight Cardboard | Low-Speed/Cost-Sensitive |
| Cold Work Die Steel | HRC 61-63 | Multi-layer Corrugated / Laminated Film | High Impact / Mid-Speed |
| Hard Alloy (Carbide) | HRA 89-93 | Battery Separators / Metal Foil | High-Speed / Wear-Heavy |
| Serrated Blades | Variable | Heavy Cardboard (Force ≥500N) | Hard Material Processing |
| Titanium Coated | Material Dependent | Adhesive Labels / Release Paper | Anti-Sticking/Clean Scenarios |
| Stainless Steel | Variable | Food Processing / Sterile Environments | Rust-Proof/Cleanroom |
The price is primarily driven by the metallurgical composition (e.g., Alloy Steel vs. Tungsten Carbide), the precision of the edge grinding (measured in microns), and any specialized surface treatments like titanium plating. Additionally, the complexity of the geometry—such as the difference between a simple straight knife and a precision circular slitting knife—impacts the manufacturing cost and final pricing.
Selection depends on the balance between impact and wear. Cold Work Die Steel (SKD-11/Cr12MoV) is superior for materials that exert high impact forces, such as heavy corrugated cardboard, due to its toughness. Hard Alloy (Tungsten Carbide) is the correct choice for speeds exceeding 100 meters/minute or when cutting highly abrasive materials like metal foil, as it offers far superior wear resistance.
Yes. While coatings like titanium plating increase the initial purchase price, they reduce "hidden" costs. By preventing material adhesion (especially in adhesive labels and release papers), coatings reduce the frequency of cleaning stops and minimize material waste caused by sticking, thereby increasing overall equipment effectiveness (OEE) and lowering the cost per unit produced.
The blade angle (typically between 15° and 23°) determines the balance between sharpness and edge strength. A smaller angle (15-20°) is used for high-speed carton molding to ensure clean cuts with minimal force. A larger angle (22-23°) is typically used for slotting knives in heavy cardboard to provide the structural integrity needed to resist chipping under high pressure.
Inspection cycles vary by material. Alloy steel blades generally require wear checks every 8 hours of operation to maintain edge precision. Hard alloy blades, due to their extreme durability, can often go 30 days between coating integrity and wear inspections, provided the material being cut remains consistent in hardness and abrasive properties.
The gap (0.03-0.1mm for thin paper; 0.1-0.3mm for thick paper) is critical for preventing burrs. Achieving and maintaining these tolerances requires higher-precision blades and more frequent calibration. Blades that can maintain their geometry over longer periods reduce the labor cost associated with gap adjustment, shifting the value from a low-cost tool to a high-precision system.
Evaluating a shearing machine blade price requires a shift in perspective from "purchase cost" to "lifecycle value." Whether utilizing the cost-effectiveness of 9CrSi for small-scale production or the extreme durability of Tungsten Carbide for high-speed industrial lines, the goal is to align the tool's metallurgical properties with the specific demands of the material and the throughput of the machine.
By prioritizing technical parameters—such as HRC/HRA hardness, blade angle, and coating integrity—over the lowest available quote, manufacturers can improve processing efficiency by 20% to 50%. The most sustainable procurement strategy is one that views the cutting blade not as a consumable commodity, but as a precision component critical to overall production quality and uptime.